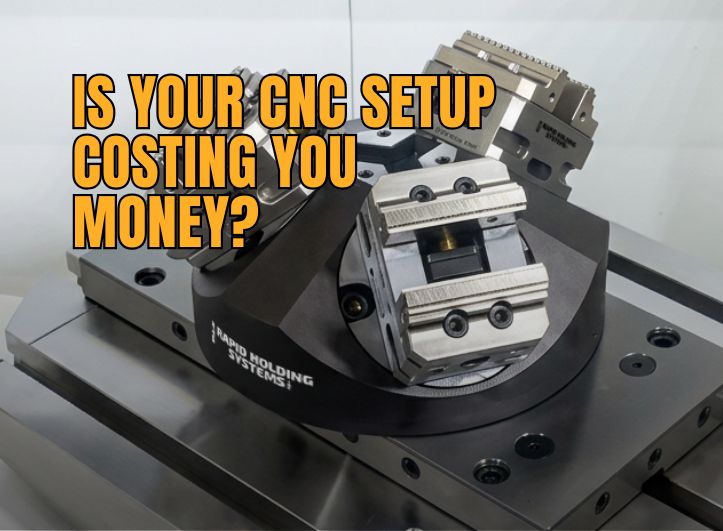
Is Your CNC Setup Costing You Money? The Problem Might Be Your Workholding 

10 Mar

There’s a mistake even experienced machine shops make: investing in top-of-the-line CNC equipment, then overlooking how the part is actually held in place.  The result is always the same — vibration, dimensional errors, rework, and lost time. And the frustrating part? The problem isn’t the machine. It’s the workholding.  Setup Time Is the Bottleneck Nobody Talks About  In CNC and EDM manufacturing, cutting time is…

read more

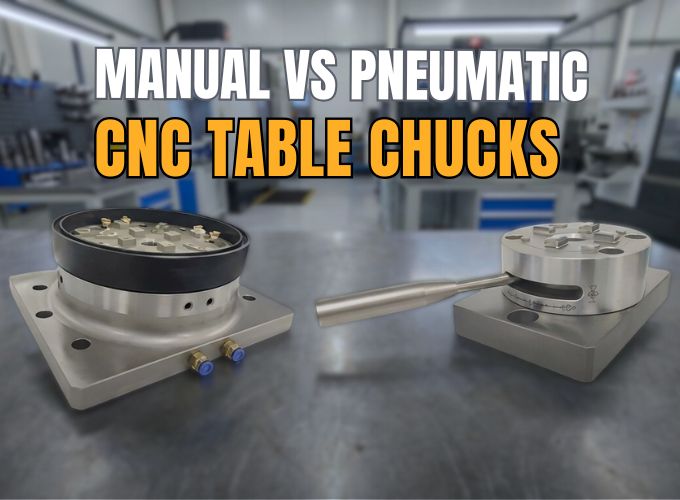
Manual vs Pneumatic CNC Table Chucks: Choosing the Right System 3R‑Compatible Setup 

10 Mar

Every minute spent re‑indicating a part is a minute not cutting. In production CNC environments that cost compounds quickly. Setup variability between shifts, inconsistent holding force during aggressive cuts and the inability to move work between machines without losing your datum translate directly into re‑work, scrap and lost tool life. A standardized pallet system solves these headaches by encoding the…

read more

Workholding Maintenance Guide: How to Protect Your CNC and EDM Precision 

02 Feb

In precision manufacturing, we all talk about tolerances, stability, and repeatability. But there’s something many shops leave out of the equation:  Maintenance of their clamping systems.  It doesn’t matter if your workholding system was a well-planned investment, compatible with the most demanding standards. Over time, any component subjected to constant cycles, coolant exposure, metal particles, or pneumatic pressure starts to change:  # Axes…

read more
,

Modular, Quick-Change, and Zero-Point: What Each Approach Does—and When It Actually Makes Sense to Use It 

27 Jan

Workholding decisions shape more than setup time. They define how stable a process is, how parts move through the shop, and whether repeatability is designed in or constantly corrected.  Modular, quick-change, and zero-point systems are often discussed together. But they solve different problems. Confusion usually starts when one approach is used to fix a problem it wasn’t designed for.  Modular…

read more
, ,

What Is a Reference System and Why It Changes How Parts Move Between Machines: CNC → EDM → Wire EDM Without Realignment 

26 Jan

In many shops, every machine treats the part as if it were new. Each operation begins by re-establishing alignment, finding zero, and redefining position. That repetition feels normal, but it quietly introduces variation.  A reference system exists to prevent that. It allows a part to move between machines while preserving the same geometric intent. The…

read more
,

Setup Time Reduction: What You Really Gain When You Move from Internal Adjustments to External Preparation

23 Jan

In many CNC shops, setup time is treated as something to be minimized at the machine. The focus is often on doing the setup faster so production can begin. What rarely gets questioned is where that setup work is actually happening.  Most setups include two very different types of work. Some tasks can only be done when the machine is stopped.…

read more

Why CNC Scrap Often Gets Blamed on the Wrong Thing 

21 Jan

When scrap appears in CNC machining, the first reaction is usually immediate. The tool gets blamed, the program gets adjusted, or the operator gets questioned. These are the most visible parts of the process.  Often, the correction seems to work. A parameter change removes the scrap, production resumes, and the issue is considered solved.  Until…

read more

Accurate Once Doesn't Mean Repeatable: Why CNC Setups Fail Over Time

21 Jan

In CNC machining, achieving tolerance once is often mistaken for proof of a good process. The part measures correctly, the setup looks clean, and production moves forward with confidence. At first glance, nothing appears unstable or worth revisiting.  But here’s the problem: accuracy at a single moment doesn’t equal repeatability over time. Many setup-related issues don’t fail during the first run. They fail quietly, after…

read more